


As environmental protection requirements continue to rise, mine water treatment systems are now facing increasingly stringent operational standards. For coal mining enterprises, achieving efficient treatment, stable operation, and energy savings and consumption reduction has become a critical challenge in the modernization of mine water recycling and reuse processes.
Recently, Xylem successfully supported a large-scale coal mine mine water advanced treatment station upgrade and renovation project in Northwest China, providing the customer with enhanced treatment capacity and optimized operational efficiency through its efficient and reliable e-MP DN125 multi-stage centrifugal pump solution.
Mine Water Treatment Upgrade
Facing three major challenges
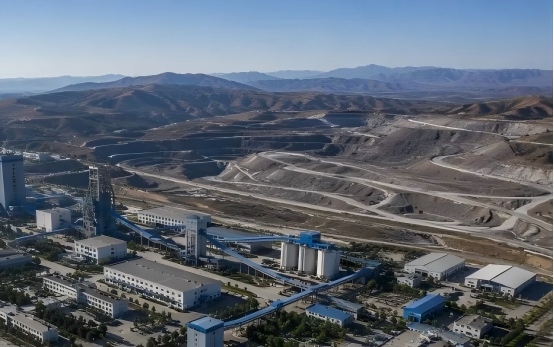
In this project, the mine water advanced treatment station plays a critical role in ensuring that mine water meets regulatory standards and is effectively recycled and reused. However, with the expansion of production scale and the tightening of environmental protection requirements, the existing equipment has gradually become inadequate to meet current operational demands.
During the project upgrade process, the client faces three major challenges:
The project deadline is tight
Mine water treatment facilities are critical to environmental compliance and production continuity; therefore, the project must complete equipment supply, installation, and commissioning within a relatively short timeframe.
Limited space
As a retrofit project, the on-site space is limited, the existing piping layout is complex, and the new equipment must be efficiently integrated with the existing system.
Severe operating conditions
The project requires a single-pump flow rate of 350 m³/h and a head of 450 m, which imposes higher demands on the equipment's performance and reliability.
e-MP DN125: Solving Upgrade Challenges
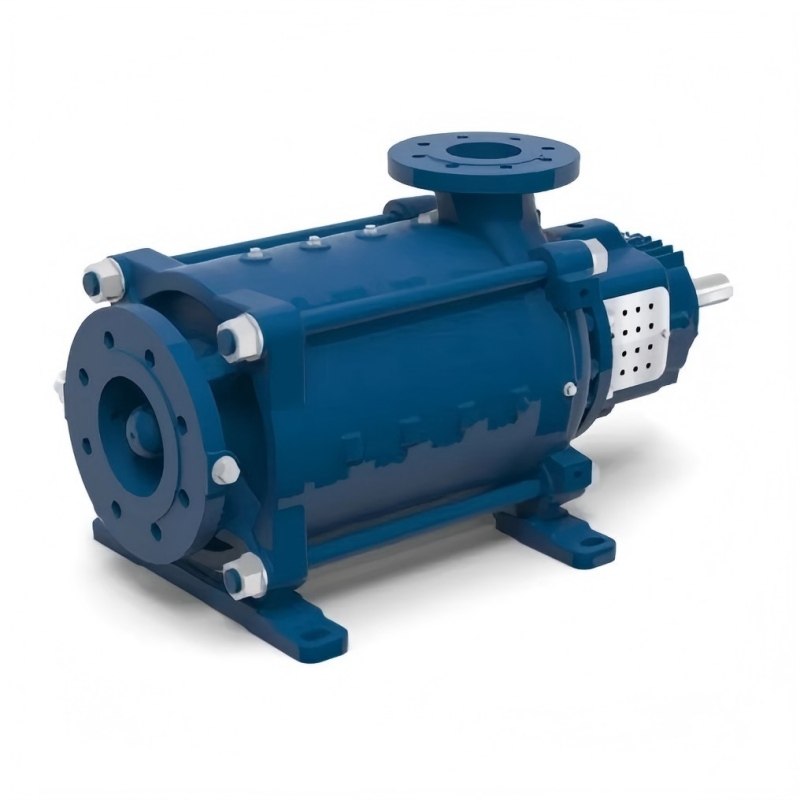
In response to project requirements, Xylem has leveraged the e-MP DN125 multi-stage centrifugal pump as its core component to deliver a comprehensive solution that balances performance, compatibility, and delivery efficiency.
 |
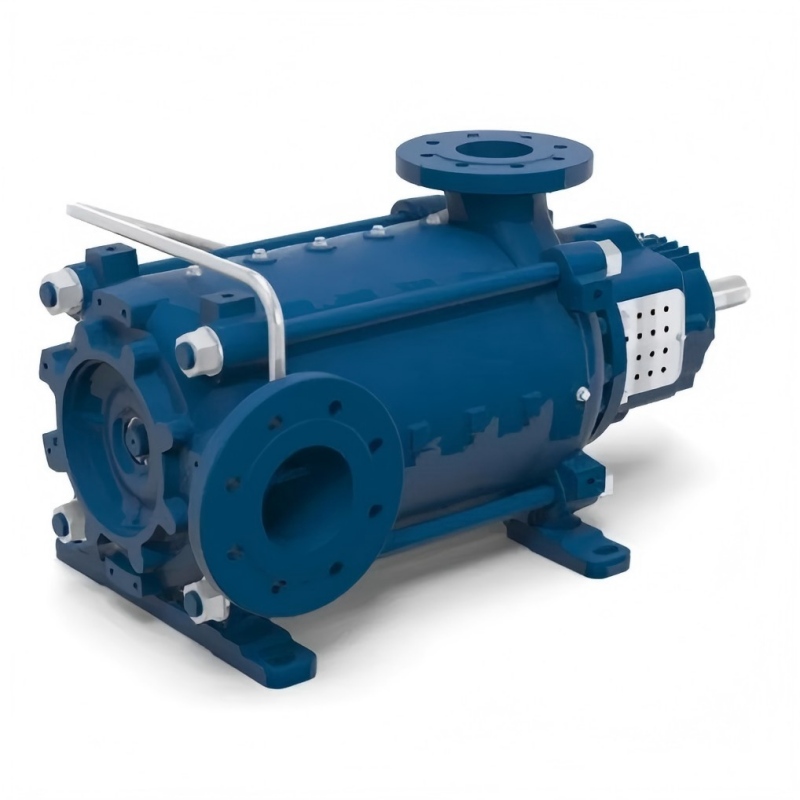 |
High efficiency and reliability, designed to meet demands for high flow rates and high head.
The e-MP series multi-stage segmented centrifugal pumps feature a well-proven hydraulic design, enabling them to meet the requirements of complex operating conditions, such as high flow rates and high head.
This project employs the MPD125B configuration, with the flow path components fabricated from 2507 duplex stainless steel, which offers excellent corrosion and wear resistance, making it suitable for transporting complex media such as mine water.
Thanks to its exceptional hydraulic performance, the equipment enables the treatment plant to maintain stable operation and enhances the overall system efficiency.
Flexible customization to adapt to complex field conditions
Given the limited space and complex piping layout, Xylem's technical team engaged in multiple rounds of solution optimization with the client.
Through customized base design and equipment layout solutions, the new equipment can be better adapted to site conditions, seamlessly integrate with the existing piping system, and effectively reduce the complexity of on-site retrofitting.
Efficient delivery to meet project milestone requirements
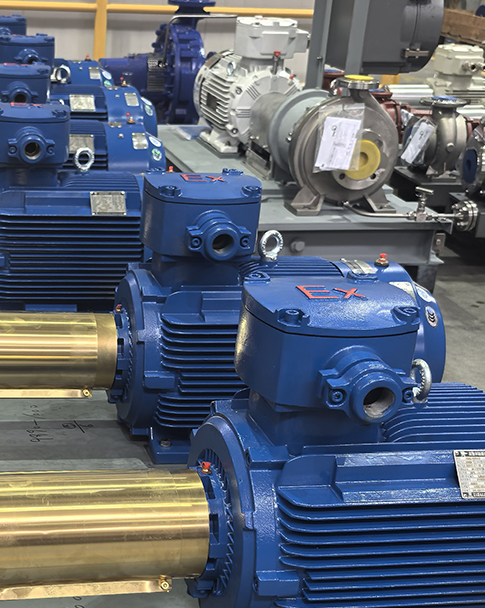
The project is equipped with a 710 kW high-voltage variable-frequency drive motor and a high-reliability transmission system. Given the tight project schedule, the Xylem team fully integrated resources from all parties, collaboratively streamlining the production, procurement, and delivery processes to ensure the project was implemented according to plan.
More than just a product
It further demonstrates our solution capabilities.
This project further validates the applicability of the e-MP platform in high-flow, high-head, and complex operating conditions. At the same time, it demonstrates Xylem's comprehensive capabilities in solution design, product customization, project collaboration, and rapid delivery. The Xylem team has consistently maintained close cooperation with its clients to jointly address engineering challenges, providing reliable support for the upgrade of mine water treatment systems.
Continuously empowering the upgrading of industrial water treatment
As industrial enterprises increasingly demand energy efficiency, environmental protection, and resource recycling, mine water treatment systems are evolving toward greater efficiency, intelligence, and sustainability.
In the future, Xylem will continue to leverage its advanced product technologies and extensive project experience to provide reliable water delivery and treatment solutions to an increasing number of industrial customers, thereby facilitating more efficient water resource management and utilization.


 IPv6 network supported.